Top 10 Ways to Inspect and Measure CNC Machined Parts?

Time:2026-09-29 Author:Liam
0%

CNC machining can produce mirror-like surfaces, tight bores, and complex profiles. Yet a part may look perfect and still fail a drawing requirement. That gap explains why inspection must be planned, repeatable, and traceable. This guide introduces the Top 10 Ways to Inspect and Measure CNC Machined Parts, from calibrated calipers to coordinate measuring machines.

Deloitte’s 2023 Global Smart Manufacturing Survey found that 86% of manufacturing leaders expect smart manufacturing to become a major competitiveness driver. That expectation depends on trustworthy measurement data. NIST’s Engineering Statistics Handbook also stresses measurement uncertainty, repeatability, and controlled variation. These principles matter on the shop floor. A worn probe, dirty datum, or warm aluminum surface can change the result. Small details matter.

So, How to inspect and measure CNC machined components? Start with the engineering drawing, not the measuring tool. Define datums, tolerances, surface requirements, and critical-to-function features. Robert Hocken, a respected coordinate-measuring-machine expert, is often quoted as saying, “A CMM is a measuring machine, not an inspection machine.” The distinction is important. Equipment collects data; trained inspectors interpret it. A steel shaft should rest on clean supports. A bore should be checked at multiple depths. Temperature should be recorded, even when production pressure is high. No inspection plan is perfect. Some measurements still deserve a second look. The methods below combine practical experience, metrology discipline, and documented evidence to reduce uncertainty without slowing every production decision.
Top 10 Ways to Inspect and Measure CNC Machined Parts?

Establish Inspection Criteria from Drawings, Tolerances, and Standards

A reliable inspection plan begins with the engineering drawing, not the measuring tool. Read the title block, revision level, material, surface finish, and unit system carefully. These details define what “acceptable” means. Identify every critical dimension and connect it to its tolerance, datum, or geometric control. A hole may meet its diameter tolerance but still fail if its position is incorrect.

Use the drawing’s stated standard for interpreting symbols, datums, and geometric tolerances. Confirm whether dimensions are expressed as limits, plus-or-minus values, or unilateral tolerances. Select instruments according to the required accuracy. A calibrated micrometer suits a tight shaft diameter, while a height gauge may verify a feature’s location from a datum surface. Record actual readings, not only pass or fail results. That record supports traceability and reveals process drift.

Tips: Inspect clean parts at a stable temperature. Control burrs before measurement. Check calibration status first. Measure critical features more than once. If readings disagree, stop and investigate instead of averaging them blindly.

Practical judgment still matters. Drawings sometimes contain unclear notes, conflicting dimensions, or unrealistic tolerance combinations. Do not silently interpret them. Ask for clarification and document the decision. I have seen a part appear compliant until the inspection sequence exposed an incorrect datum setup. The mistake was not the instrument. It was the inspection logic. Rechecking assumptions may feel slow, but it prevents confident errors and unnecessary rework.

Top 10 Ways to Inspect and Measure CNC Machined Parts

Typical instrument display resolution for common dimensional checks

Typical resolutions shown: 1 µm = 0.001 mm; 10 µm = 0.01 mm. Actual instrument specifications vary. Resolution is the smallest displayed increment, not measurement accuracy. Set acceptance limits from the engineering drawing, applicable tolerances, and required standards; select a method with suitable measurement uncertainty.

Prepare the Part and Select Calibrated Measurement Tools

Before measuring a CNC machined part, remove chips, coolant, and burrs from every critical surface. A single trapped chip can change a reading by several micrometres. Let the part and tools reach a stable temperature near 20°C, the reference temperature defined by ISO 1. Handle precision parts with clean gloves. Warm hands can affect small dimensions.

Select tools according to the tolerance, not convenience. A micrometer suits outside diameters, while a bore gauge or calibrated internal micrometer suits holes. Verify each tool’s calibration status, resolution, and zero before use. The National Institute of Standards and Technology explains that measurement uncertainty includes both statistical and non-statistical components (NIST Technical Note 1297). Record the tool ID, calibration date, temperature, operator, and measured value. Small details matter.

Use a certified reference standard to check repeatability. Measure the same feature several times, then compare the spread. If results vary, inspect alignment, contact pressure, surface finish, and fixture stability. Do not force the tool. That habit is common, and it is wrong. NIST Technical Note 1297 also recommends expanded uncertainty using coverage factor k=2, which generally represents about 95% coverage under normal distribution assumptions. I still question this shortcut when the process is unstable. A clean setup is valuable, but it cannot repair poor measurement discipline.

Measure Dimensions with Calipers, Micrometers, and Gauges

When inspecting CNC machined parts, dimensional measurement should begin with a clean, stable surface. Remove chips, oil, and visible burrs before touching the feature. A thin burr can change a reading enough to create an unnecessary rejection. Even an experienced operator can miss this detail during a busy production shift.

Calipers work well for general dimensions, step depths, and outside diameters. Close the jaws gently, keep them square, and take readings at several positions. Micrometers provide finer control for shafts, walls, and critical thicknesses. Apply consistent pressure with the measuring mechanism, not extra hand force.

Temperature changes can affect both the part and the tool. Allow them to reach the same workshop temperature. Small errors matter.

Gauges offer fast, repeatable checks when a feature has a defined limit. A plug gauge can verify an internal diameter, while a ring gauge checks an external diameter. Confirm the gauge’s calibration status before use, and inspect it for wear or damage. Record actual measurements instead of marking only “pass” or “fail.” That record helps reveal tool drift and process variation.

I have occasionally measured a part twice and obtained different results because my contact angle changed. That mistake deserves attention, not concealment. Repeating the measurement with a consistent method usually exposes the cause.

Inspect Geometry, Surface Finish, and Complex Features

Top 10 Ways to Inspect and Measure CNC Machined Parts

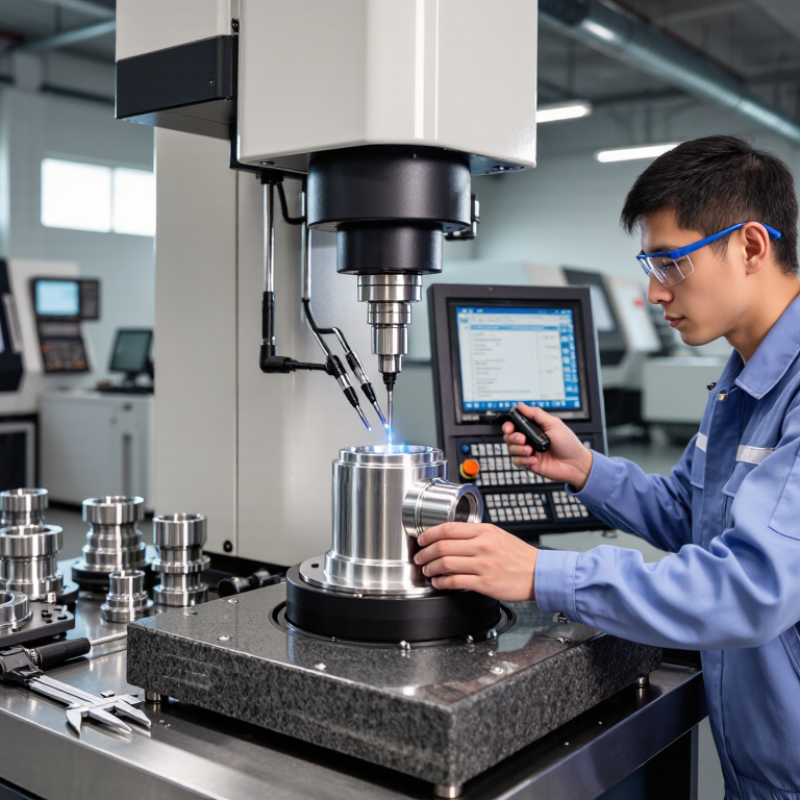
Reliable inspection starts with the drawing, datums, and tolerance requirements. Use calipers for quick checks, then verify critical dimensions with micrometers. A coordinate measuring machine can confirm hole positions, flatness, and true geometric relationships. Surface plates help reveal rocking, warping, or uneven contact. Gauge pins are useful for checking internal diameters, while thread gauges verify pitch and fit. Measure more than one location. Machining variation is rarely uniform.

Surface finish needs separate attention. A profilometer records roughness values, instead of relying only on touch or visual judgment. Compare the measured result with the specified Ra value and machining direction. An optical comparator can inspect profiles, radii, chamfers, and small external features. For deep cavities, magnified visual inspection or a borescope may reveal burrs, tool marks, and trapped chips. Complex parts often need multiple setups, and alignment errors can create false results.

Tips: Clean the part before measuring. Let it reach room temperature. Record the instrument, method, and result. Inspect every critical feature, not only the easiest ones. No inspection plan is perfect. I have seen excellent dimensions fail because a hidden burr changed assembly force. Review unclear tolerances with engineering before accepting the part. Recheck unusual readings, especially when measurement pressure, fixture movement, or operator technique may influence the result.

Top 10 Ways to Inspect and Measure CNC Machined Parts: Geometry, Surface Finish, and Complex Features

Inspection Method Best For What It Measures or Checks Practical Notes
1. Coordinate Measuring Machine (CMM) Prismatic parts, datum relationships, and complex 3D geometry Point coordinates, dimensions, angles, hole locations, profiles, and geometric tolerances Can use contact probes or non-contact sensors. Results depend on probe access, part fixturing, calibration, and a suitable measurement program.
2. Optical Comparator or Profile Projector Small profiles, contours, radii, and edges Magnified two-dimensional outlines and selected linear or angular dimensions Useful for comparing a projected profile with a drawing or overlay. It does not directly verify hidden or three-dimensional features.
3. Vision Measuring System Small parts and features that are difficult to contact Edges, centers, distances, diameters, and two-dimensional profiles from camera images Lighting, focus, edge-detection settings, and surface contrast affect results. Appropriate for accessible, visible features.
4. Micrometers and Calipers Routine shop-floor dimensional checks Outside, inside, and depth dimensions such as thicknesses, diameters, and step heights Select a tool with suitable range and resolution. Calipers are versatile; micrometers generally provide more controlled contact for suitable dimensions.
5. Bore Gauges and Plug Gauges Holes, bores, and internal diameters Bore size, taper, ovality, or whether a feature falls within specified limits Set comparative bore gauges against a reference. Go/no-go plug gauges provide a fast limit check but do not report the actual diameter.
6. Height Gauge on a Surface Plate Heights, steps, and feature locations from a reference plane Vertical dimensions and selected X or Y positions when used with suitable accessories Clean the surface plate and part datum surfaces, and secure the workpiece consistently. The setup and datum choice influence the result.
7. Dial Indicator or Test Indicator Runout, alignment, flatness checks, and machine setup Relative displacement as a part or indicator moves across a surface Often used while rotating a shaft or sweeping a face. It reveals variation relative to the setup, rather than automatically identifying its cause.
8. Surface Roughness Tester Functional or specified machined surfaces Profile roughness parameters such as Ra or Rz, depending on the instrument and selected standard Measure in the specified direction and location, using an appropriate cutoff and filter. A single reading may not represent an entire surface.
9. Thread Gauges Internal and external threaded features Thread acceptance against specified pitch diameter limits using suitable limit gauges Choose gauges for the thread form, size, and tolerance class. A limit gauge checks conformity; it is not a substitute for a full thread measurement when actual values are required.
10. 3D Optical Scanning Freeform surfaces and comparison with a CAD model A point cloud or mesh used to assess surface shape, deviations, and overall geometry Line of sight, surface reflectivity, scan coverage, and alignment affect results. Critical dimensions may need confirmation with a calibrated contact method.

Record Results, Assess Conformance, and Address Deviations

For each CNC machined part, record the measurement beside its drawing requirement, not on a separate note that can be misplaced. Include the part number, revision, inspection date, instrument ID, and sample size. Write down actual readings, such as a 24.98 mm bore against a 25.00 ± 0.05 mm tolerance. “Pass” alone hides useful information. Keep it traceable.

Compare each reading with the specified tolerance and datum scheme. A feature may fall within its size limits yet still fail its position requirement. Check that the measuring instrument suits the feature and has a current calibration status. For a tight bore, temperature and measuring technique can shift the result; let the part and gauge stabilize before recording. A hurried second reading may disagree. That deserves a closer look.

When a result is out of tolerance, identify and segregate the affected parts, then document the measured value and inspection method. Review tool offsets, setup notes, and earlier measurements to see whether the deviation began gradually or appeared suddenly. Recheck with a suitable method before deciding the result is real. Record who approved any disposition and why; never quietly replace an original reading. Sometimes the cause remains uncertain. Note that plainly, investigate the process, and inspect additional parts when the risk warrants it.

FAQS

How should a machined part be prepared before measurement?

Clean the part on a stable surface. Remove chips, oil, and visible burrs. A tiny burr can cause rejection.

When are calipers suitable for inspection?

Use calipers for general dimensions, step depths, and outside diameters. Keep the jaws square and close them gently.

Why are micrometers used for critical dimensions?

Micrometers provide finer control for shafts, walls, and critical thicknesses. Apply steady measuring pressure, not extra hand force.

Can temperature affect dimensional readings?

Yes. Let the part and instrument reach the same workshop temperature. Small temperature differences can change results.

How can gauges support fast inspection?

Gauges provide quick, repeatable checks against defined limits. Inspect their calibration status, wear, and possible damage before use.

Why should measurements be taken at several locations?

Machining variation is rarely uniform. Check multiple positions to reveal taper, warping, or inconsistent geometry.

What tools can inspect complex features?

A coordinate measuring machine can check hole positions, flatness, and geometric relationships. Optical inspection can reveal profiles, radii, and chamfers.

How should surface finish be evaluated?

Use a roughness instrument to record the surface value. Compare it with the specified Ra requirement and machining direction.

What should be recorded during inspection?

Record the instrument, method, location, and actual measurement. “Pass” or “fail” alone hides useful process information.

What should happen when two readings disagree?

Repeat the measurement with consistent pressure and contact angle. I have made this mistake. The method may need review.

Conclusion

Effective inspection begins with clearly defined acceptance criteria drawn from engineering drawings, specified tolerances, and applicable quality standards. Before taking measurements, clean and stabilize the part, confirm the measurement conditions, and select calibrated tools suited to its material, size, and required precision. A consistent setup helps reduce handling errors and makes results easier to compare.

How to inspect and measure CNC machined components? Use calipers, micrometers, and gauges to verify key dimensions, then examine geometry, surface finish, and complex features with appropriate inspection methods. Record measurements alongside the relevant requirements, assess whether each result conforms, and investigate any deviation before deciding on corrective action. This organized process supports reliable decisions, clear documentation, and consistent quality throughout production.
Liam

Liam

Liam is a dedicated marketing professional with a profound expertise in the industry, where he excels at highlighting the unique advantages of our core products. With a keen understanding of market trends and consumer needs, Liam frequently updates our company’s professional blog, providing......